Vietnam Galvanized Steel Producer Adds Continuous Hot Dip Galvanizing and Galvalume Line for Export Coils
A Vietnamese coated-steel producer has put a new continuous hot-dip galvanizing and galvalume production line into operation, targeting an annual capacity of 300,000 MT to serve export markets in ASEAN, the Middle East and North America. The line combines zinc and zinc-aluminium alloy coating in one process train, allowing the producer to switch product mix according to order book and alloy price movements.
Client Background
The client operates a cold-rolling and coating plant in southern Vietnam supplying galvanized coil to roofing sheet manufacturers, steel pipe and tube makers, and general construction suppliers. With export demand growing, its existing line — limited in width and coating range — could no longer cover the wide, thin-gauge orders that overseas buyers were requesting, and changeover between zinc and aluminium-zinc coating was costly and slow.
The Challenge
- Export orders demanded widths up to 1,650 mm and thin gauges down to 0.1 mm
- Buyers required coating weights across a very wide 60–275 g/m² band, held to tight tolerance
- Frequent switching between zinc and galvalume products without long downtime
- Deep-drawing and structural grades required consistent annealing and flatness
- Energy and emissions targets under Vietnam's tightening environmental rules
The Solution
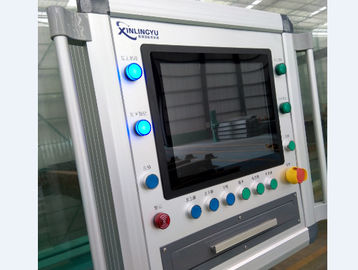
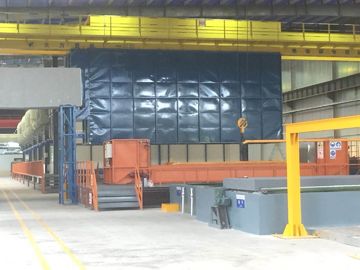
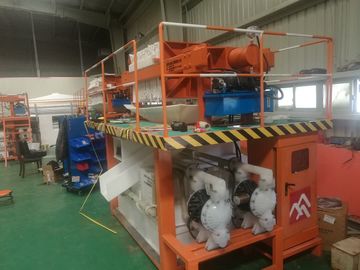
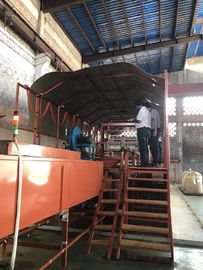
We delivered a fully continuous line that plates a layer of zinc or zinc-aluminium alloy onto the strip at high temperature while the strip runs uninterrupted from entry to exit. The configuration comprises uncoiler, welder, strip storage, degreasing section equipment, continuous annealing furnace, zinc pot, air knife, skin pass, tension leveler, oiler, shear and recoiler, together with all auxiliary equipment needed for round-the-clock operation.
The line accepts cold-rolled hard-state coil in SPCC and SPCD, thickness 0.1–2.5 mm, width 650–1,650 mm, with coil weights up to 25 tonnes. Annealing reduction in the continuous furnace prepares the strip surface for coating, and the air knife system holds coating weight anywhere in the 60–275 g/m² double-side range with ±5 g/m² adjustability — giving the producer the flexibility to run light-gauge roofing product and heavy-coating structural material on the same line. Skin pass and tension leveling secure flatness and mechanical properties for CQ, DQ and DDQ grades.
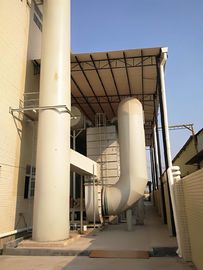
To cut operating cost and meet environmental targets, the furnace is fitted with a waste-gas heat recovery system that reuses exhaust heat, and the coating section is enclosed so that fume is captured and treated rather than released into the workshop. The result is lower energy consumption per tonne and a cleaner, more stable working environment across three-shift production.
Line Configuration
| Process Section | Function |
|---|
| Uncoiler & welder | Continuous strip feeding and coil joining |
| Strip storage | Keeps the line running during coil changes |
| Degreasing section equipment | Cleans strip surface before furnace entry |
| Continuous annealing furnace | Annealing reduction for coating adhesion |
| Zinc pot & air knife | Zinc or zinc-aluminium coating with precise weight control |
| Skin pass & tension leveler | Flatness, surface finish and property control |
| Oiler, shear, recoiler | Oiling, cutting and finished coil take-up |
Technical Specifications
| Parameter | Specification |
|---|
| Line type | Continuous hot-dip galvanizing / galvalume line |
| Raw material | Cold-rolled hard-state steel coil, SPCC / SPCD |
| Strip thickness | 0.1 – 2.5 mm |
| Strip width | 650 – 1,650 mm |
| Coating weight | 60 – 275 g/m² (double-side) ±5 g/m² adjustable |
| Coil weight | Max 25 tonnes |
| Product grade | CQ, DQ, DDQ |
| Annual capacity | 100,000 – 300,000 MT/Y (300,000 MT/Y configured) |
| Energy saving | Heat recovery system from waste gas |
| Line functions | Annealing reduction, galvanizing, finishing, straightening |
Results & Benefits
- Full 650–1,650 mm width and 0.1–2.5 mm gauge coverage opened export-grade order books.
- Coating weight adjustable across 60–275 g/m² with ±5 g/m² tolerance met buyer specifications.
- Zinc and galvalume products run on the same train, so the producer follows market demand quickly.
- Waste-gas heat recovery reduced furnace energy consumption per tonne of coated coil.
- Enclosed, fume-captured coating section supported environmental compliance and shop-floor safety.
- CQ/DQ/DDQ capability widened supply to roofing, tube and appliance customers.
Conclusion
With the new continuous galvanizing and galvalume line, the Vietnamese producer moved from a narrow domestic supplier to a 300,000 MT/Y export-capable coated steel maker. The combination of wide-breadth capability, tight coating control, dual-product flexibility and heat-recovery energy savings gives it a cost position and product range that competing regional mills will find hard to match.

 Ihre Nachricht muss zwischen 20 und 3.000 Zeichen enthalten!